Sponsored article
How to Plan Buffers Between Roasting, Storage and Packaging in Coffee Production
- Why Is a Buffer Needed After Coffee Roasting?
- How Should Storage Be Matched to the Roasting Cycle?
- How Much Buffer Capacity Is Needed Before Packaging?
- How Do You Identify the Bottleneck in a Coffee Production Line?
- Why Should Buffer Capacity Not Be Used to Hide a Bottleneck?
- What Does a Well-Designed Coffee Flow Provide?
- FAQ
Coffee production does not end when roasted beans leave the roasting drum. Before the coffee reaches its final packaging, it may pass through cooling, intermediate storage, quality control and internal transport. Depending on the production process and packaging system, there may also be a defined holding period before packing.
Read more: Why choose a wholesale mushroom supplier for a diverse culinary offering?
If the capacities of these stages are not properly coordinated, even an efficient coffee roaster can create material build-up further down the line. Buffers help separate processes that operate at different speeds and maintain a smooth product flow without unnecessarily increasing work-in-progress inventory.
Read more: What Determines Tray Grip in Wet Service, and How Is Its Surface Texture Created?
Why Is a Buffer Needed After Coffee Roasting?
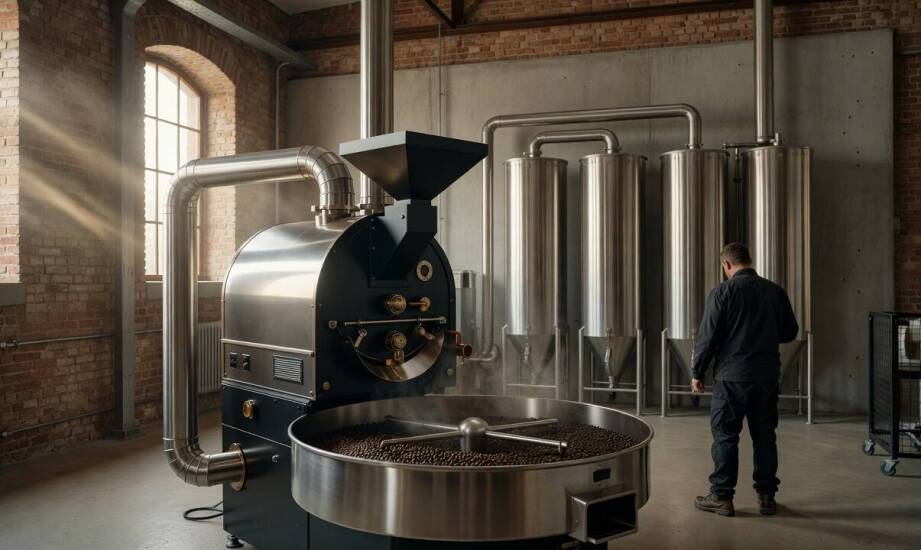
After roasting, coffee beans need to be cooled quickly and transferred to the next stage without mixing batches or compromising traceability.
The purpose of a buffer is to separate the different operating rhythms of the roaster, storage section and packing equipment rather than simply to accumulate a large quantity of coffee.
For coffee manufacturers, this means looking at the capacity of the complete production line rather than focusing on the performance of a single machine.
If the roaster completes batches faster than the packaging section can accept them, an appropriately designed intermediate storage system is required. Its capacity should take into account:
batch size;
roasting frequency;
the required holding time before packaging;
the actual throughput of the next production stage.
A well-designed buffer prevents short-term differences in capacity from immediately stopping upstream equipment.
How Should Storage Be Matched to the Roasting Cycle?
A buffer does not necessarily have to be one large storage vessel. Depending on the scale and layout of the plant, intermediate storage may consist of separate containers, silos or other storage and handling solutions that keep individual batches under control.
Managing the flow of beans is the key consideration. Insufficient buffer capacity can force an upstream process to stop, while excessive capacity increases work-in-progress inventory and may make batch sequencing more difficult.
When planning a coffee production line, the entire technological process should therefore be considered as one system.
Coffed offers commercial coffee roasters as well as equipment for coffee production lines, including silo storage and coffee packing solutions. The company’s current portfolio illustrates why roasting, storage and packaging capacities should be considered together rather than treated as unrelated machine specifications.
How Much Buffer Capacity Is Needed Before Packaging?
Buffer capacity is best determined by analysing product flow.
The first step is to establish how much roasted coffee can be produced over a defined period and how much coffee the packaging section can handle during the same time.
The buffer should absorb temporary differences between these two capacities.
The calculation should also take account of planned interruptions such as:
packaging format changes;
machine cleaning;
production changeovers;
short packaging-line stops;
transitions between different products or roast profiles.
This does not mean that the largest possible buffer is automatically the best solution. Excessive intermediate stock increases the amount of product waiting between operations and can make production scheduling more complicated.
Where several blends, origins or roast profiles are processed, storage should also be organised so that batches remain clearly separated before packaging.
How Do You Identify the Bottleneck in a Coffee Production Line?
Planning should begin with the actual operating capacity of every stage rather than catalogue performance figures alone.
The analysis should include:
loading the roaster;
roasting time;
cooling;
transferring the coffee;
filling and emptying intermediate storage;
weighing or dosing;
packaging.
The slowest stage determines the effective throughput of the complete line.
Increasing roasting capacity will not necessarily increase the number of finished packs produced if the packaging section remains the limiting factor.
It is useful to analyse several operating scenarios, including a typical production day, peak production and periods with frequent product changeovers.
A buffer can then be sized to absorb short-term fluctuations in flow rather than being used to hide a permanent mismatch between machine capacities.
Why Should Buffer Capacity Not Be Used to Hide a Bottleneck?
A production buffer is useful when neighbouring processes operate in different cycles or when one stage requires short, predictable interruptions.
It is less effective when there is a permanent capacity imbalance.
For example, if a roasting section can consistently produce significantly more coffee per hour than the packaging line can handle, increasing intermediate storage only delays the point at which production will eventually have to slow down.
Buffer storage should provide operational flexibility, not compensate indefinitely for an undersized downstream process.
For this reason, the buffer calculation should be combined with an assessment of equipment throughput and planned operating schedules.
What Does a Well-Designed Coffee Flow Provide?
Buffers between roasting, storage and packaging should reflect the actual production rhythm and batch sizes.
Their purpose is to create flexibility between operations while maintaining control over the coffee, batch identity and production sequence.
A well-balanced flow can help:
reduce unnecessary waiting between stages;
prevent short packaging interruptions from immediately stopping roasting;
maintain clear batch separation;
improve production scheduling;
limit unnecessary work-in-progress inventory.
Analysing the complete journey of the beans makes it easier to select appropriate intermediate capacities and identify where production is genuinely being restricted.
The objective is not to maximise storage but to create enough flexibility for individual stages of the line to work together efficiently.
FAQ
Should a Buffer Have a Higher Capacity Than the Coffee Roaster?
This cannot be determined by comparing a single parameter. Buffer capacity and discharge rate should be matched to batch size, roasting frequency and the throughput of downstream production stages.
The required capacity depends on the difference between the amount of coffee entering and leaving the buffer over time.
Where Is the Best Place for a Buffer in a Coffee Production Line?
Buffers are particularly useful between stages that operate at different speeds or where one process is subject to periodic interruptions.
The exact location should be determined by analysing the product flow from roasting through intermediate storage to final packaging.
Does a Larger Intermediate Storage System Always Improve Efficiency?
No. Excessive work-in-progress inventory can make batch management and production scheduling more difficult and does not eliminate the actual bottleneck in the line.
The cause and duration of production interruptions should be identified first, and the buffer should then be sized according to the real difference in throughput.
You might be interested
Why choose a wholesale mushroom supplier for a diverse culinary offering?
Birettas in Sacred Art: Meaning, Form, and Spiritual Message
What Do USP Stability Studies Conducted by Vitamin K2 MK-7 Manufacturers Involve?